INQUIRY

Manufacturing

5 Steel Plate
Steel Plate Manufacturing Process

  1. Rolling
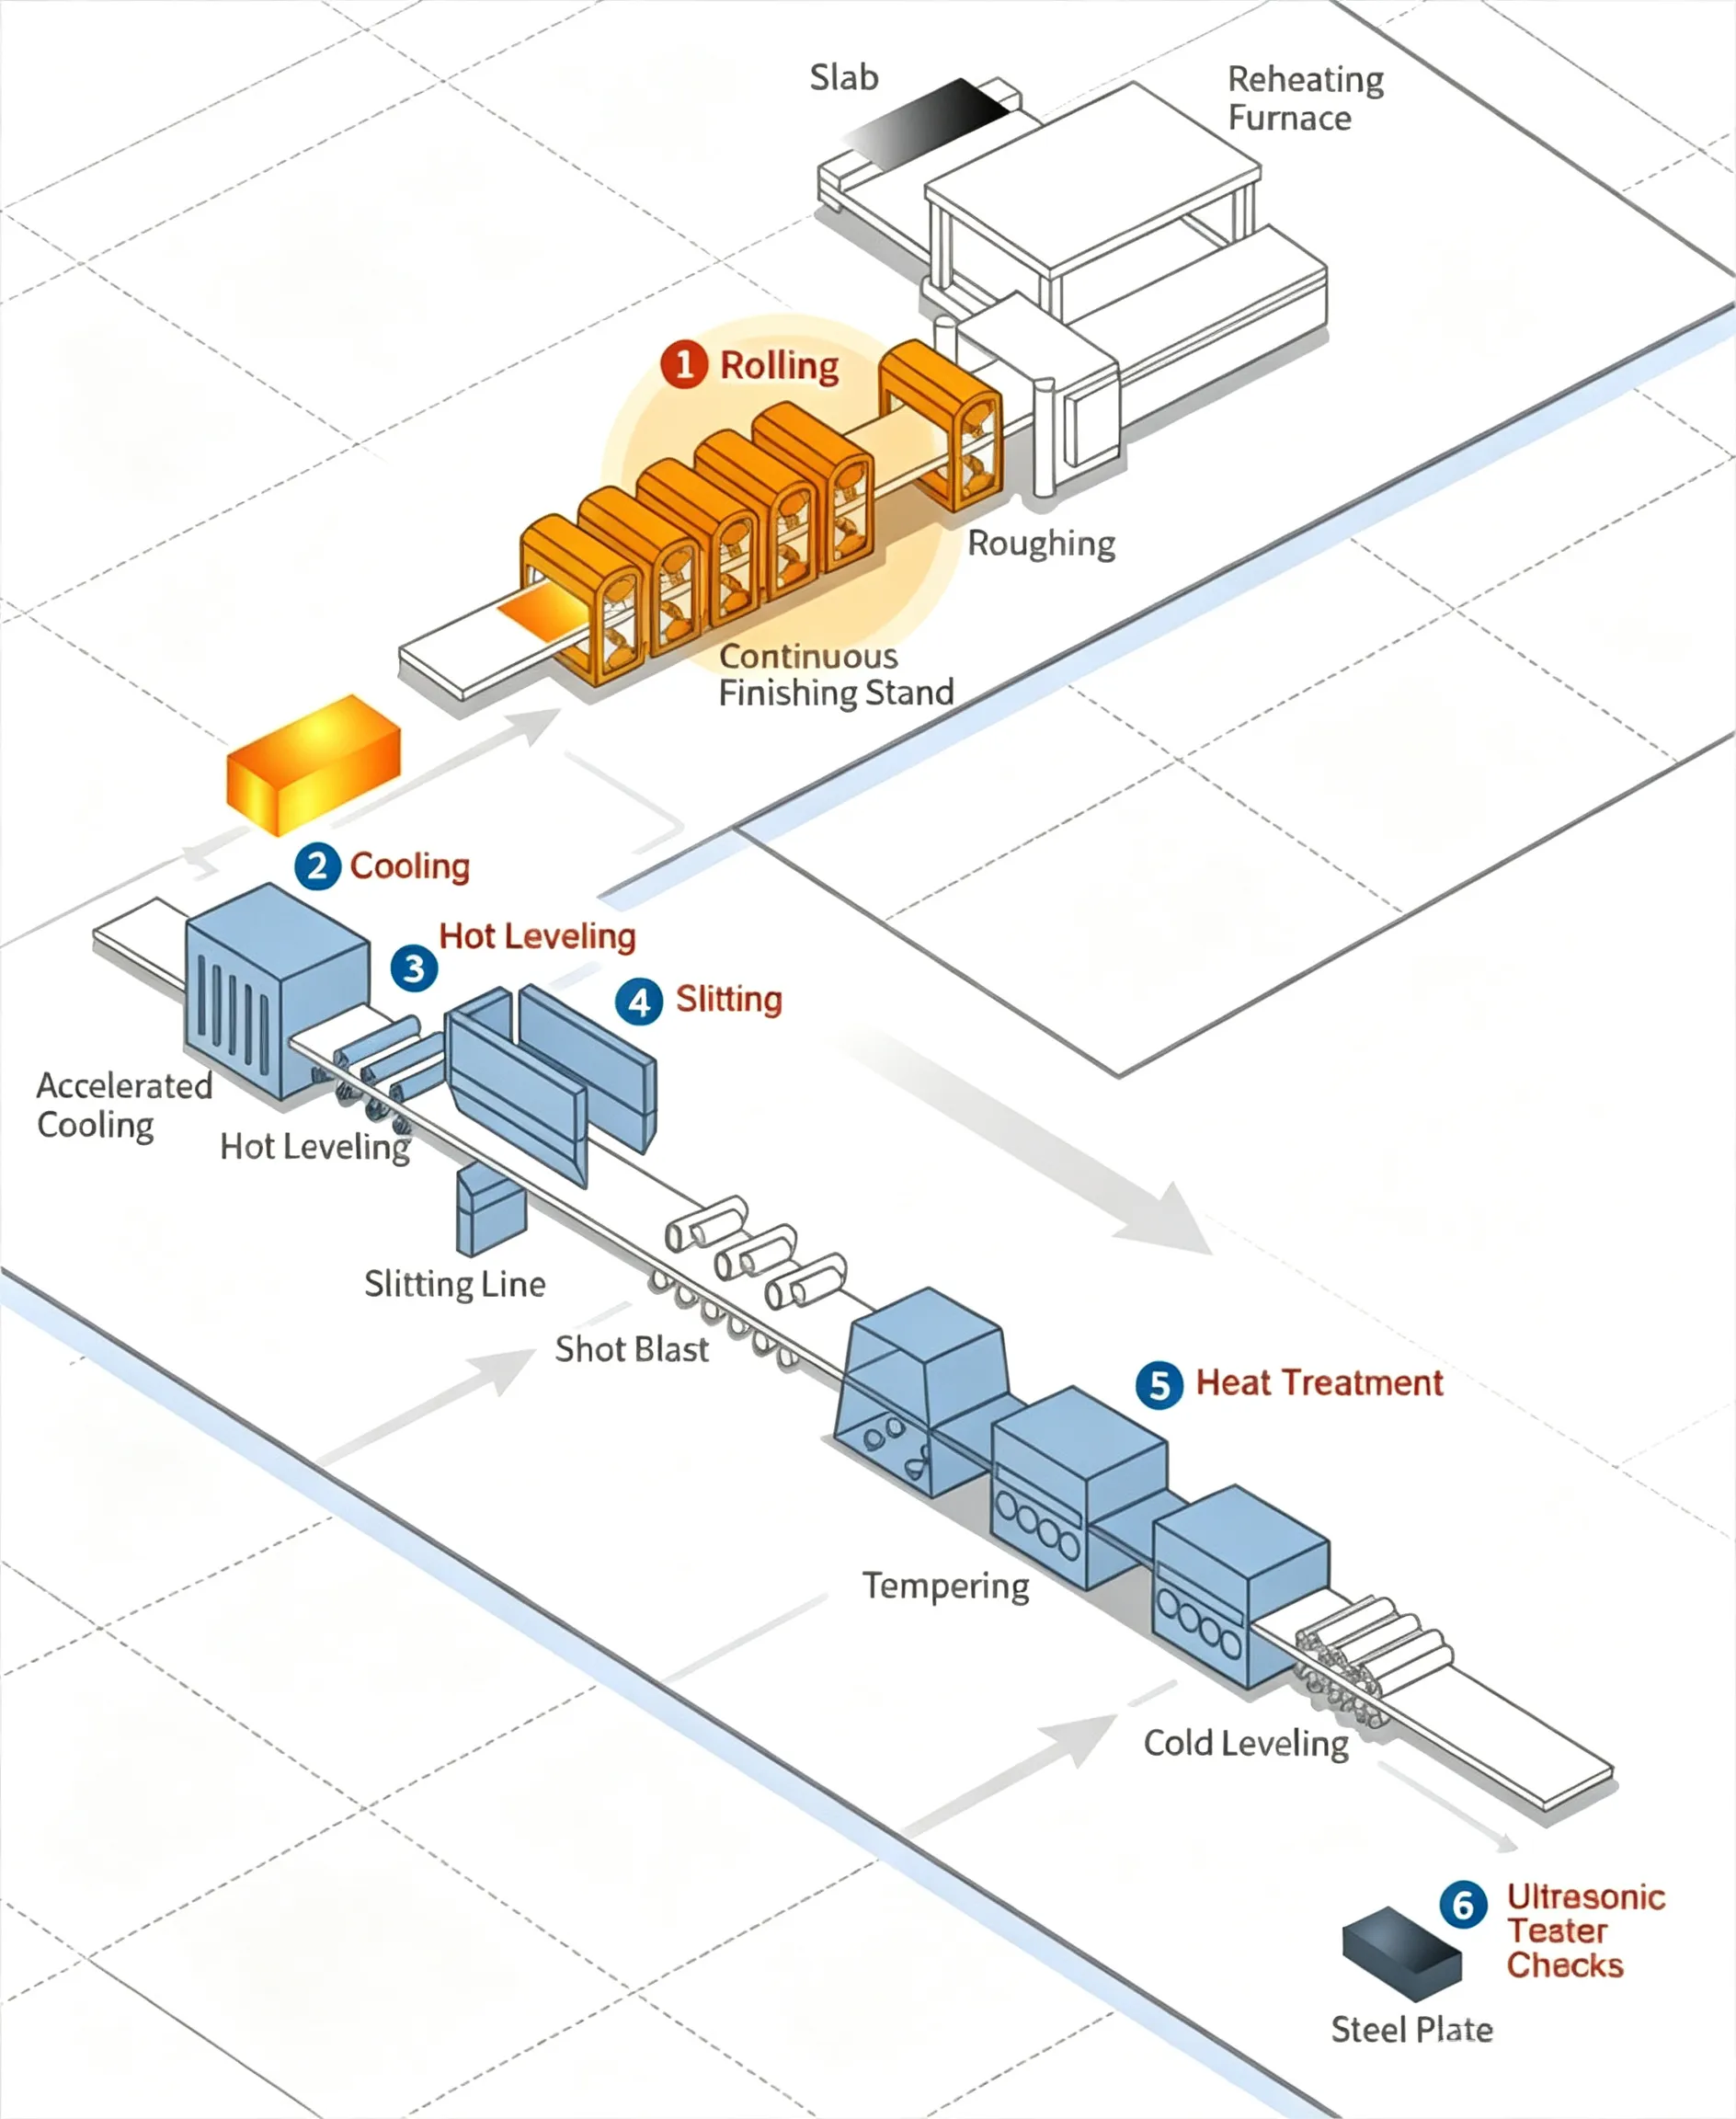
    Steel plates are processed through a 4-high reversible finishing mill with a maximum rolling force of 7,000 tons, enabling precise thickness control and minimizing internal defects even in heavy and thick plates. Advanced Automatic Gauge Control (AGC) and Automatic Shape Control (ASC) systems effectively reduce thickness deviation, improve flatness, and ensure consistent plate quality.
  2. Accelerated Cooling
    The advanced cooling system enables the production of high-strength steel plates through controlled rolling and accelerated cooling processes, eliminating the need for additional heat treatment in certain applications. Utilizing a suction-type mist cooling system, the process provides high cooling efficiency and maintains a uniform temperature distribution across the plate width, significantly improving mechanical properties and reducing quality variations.
  3. Hot Leveling
    Hot leveling is performed to eliminate residual stresses generated during rolling, improving plate flatness, dimensional stability, and overall product quality. This process ensures that finished steel plates meet strict requirements for precision and surface performance.
  4. Cutting and Dimensioning
    After cooling, steel plates undergo dimensional inspection before being cut to specified widths and lengths according to customer requirements, steel grade, and thickness. Advanced mechanical shearing and flame cutting technologies are applied to achieve high dimensional accuracy. Cutting parameters, including air knife clearance and gas torch nozzle specifications, are precisely controlled to ensure superior cutting quality and consistency.
  5. Heat Treatment
    To achieve the required metallurgical structure and mechanical properties, steel plates undergo customized heat treatment after surface descaling by shot blasting equipment. Advanced non-oxidizing radiation tube-type furnaces are utilized to prevent secondary oxidation and produce clean, scale-free heat-treated plates with excellent performance and reliability.
  6. Ultrasonic Testing and Quality Inspection
    Advanced ultrasonic testing equipment is employed to detect internal defects such as blow holes, pipes, laminations, and other discontinuities within the steel plate. This comprehensive inspection process ensures superior internal quality and guarantees that products meet stringent customer specifications and international standards.
4 Electrical Steel
Electrical Steel Manufacturing Process

  1. Preliminary Annealing and Descaling
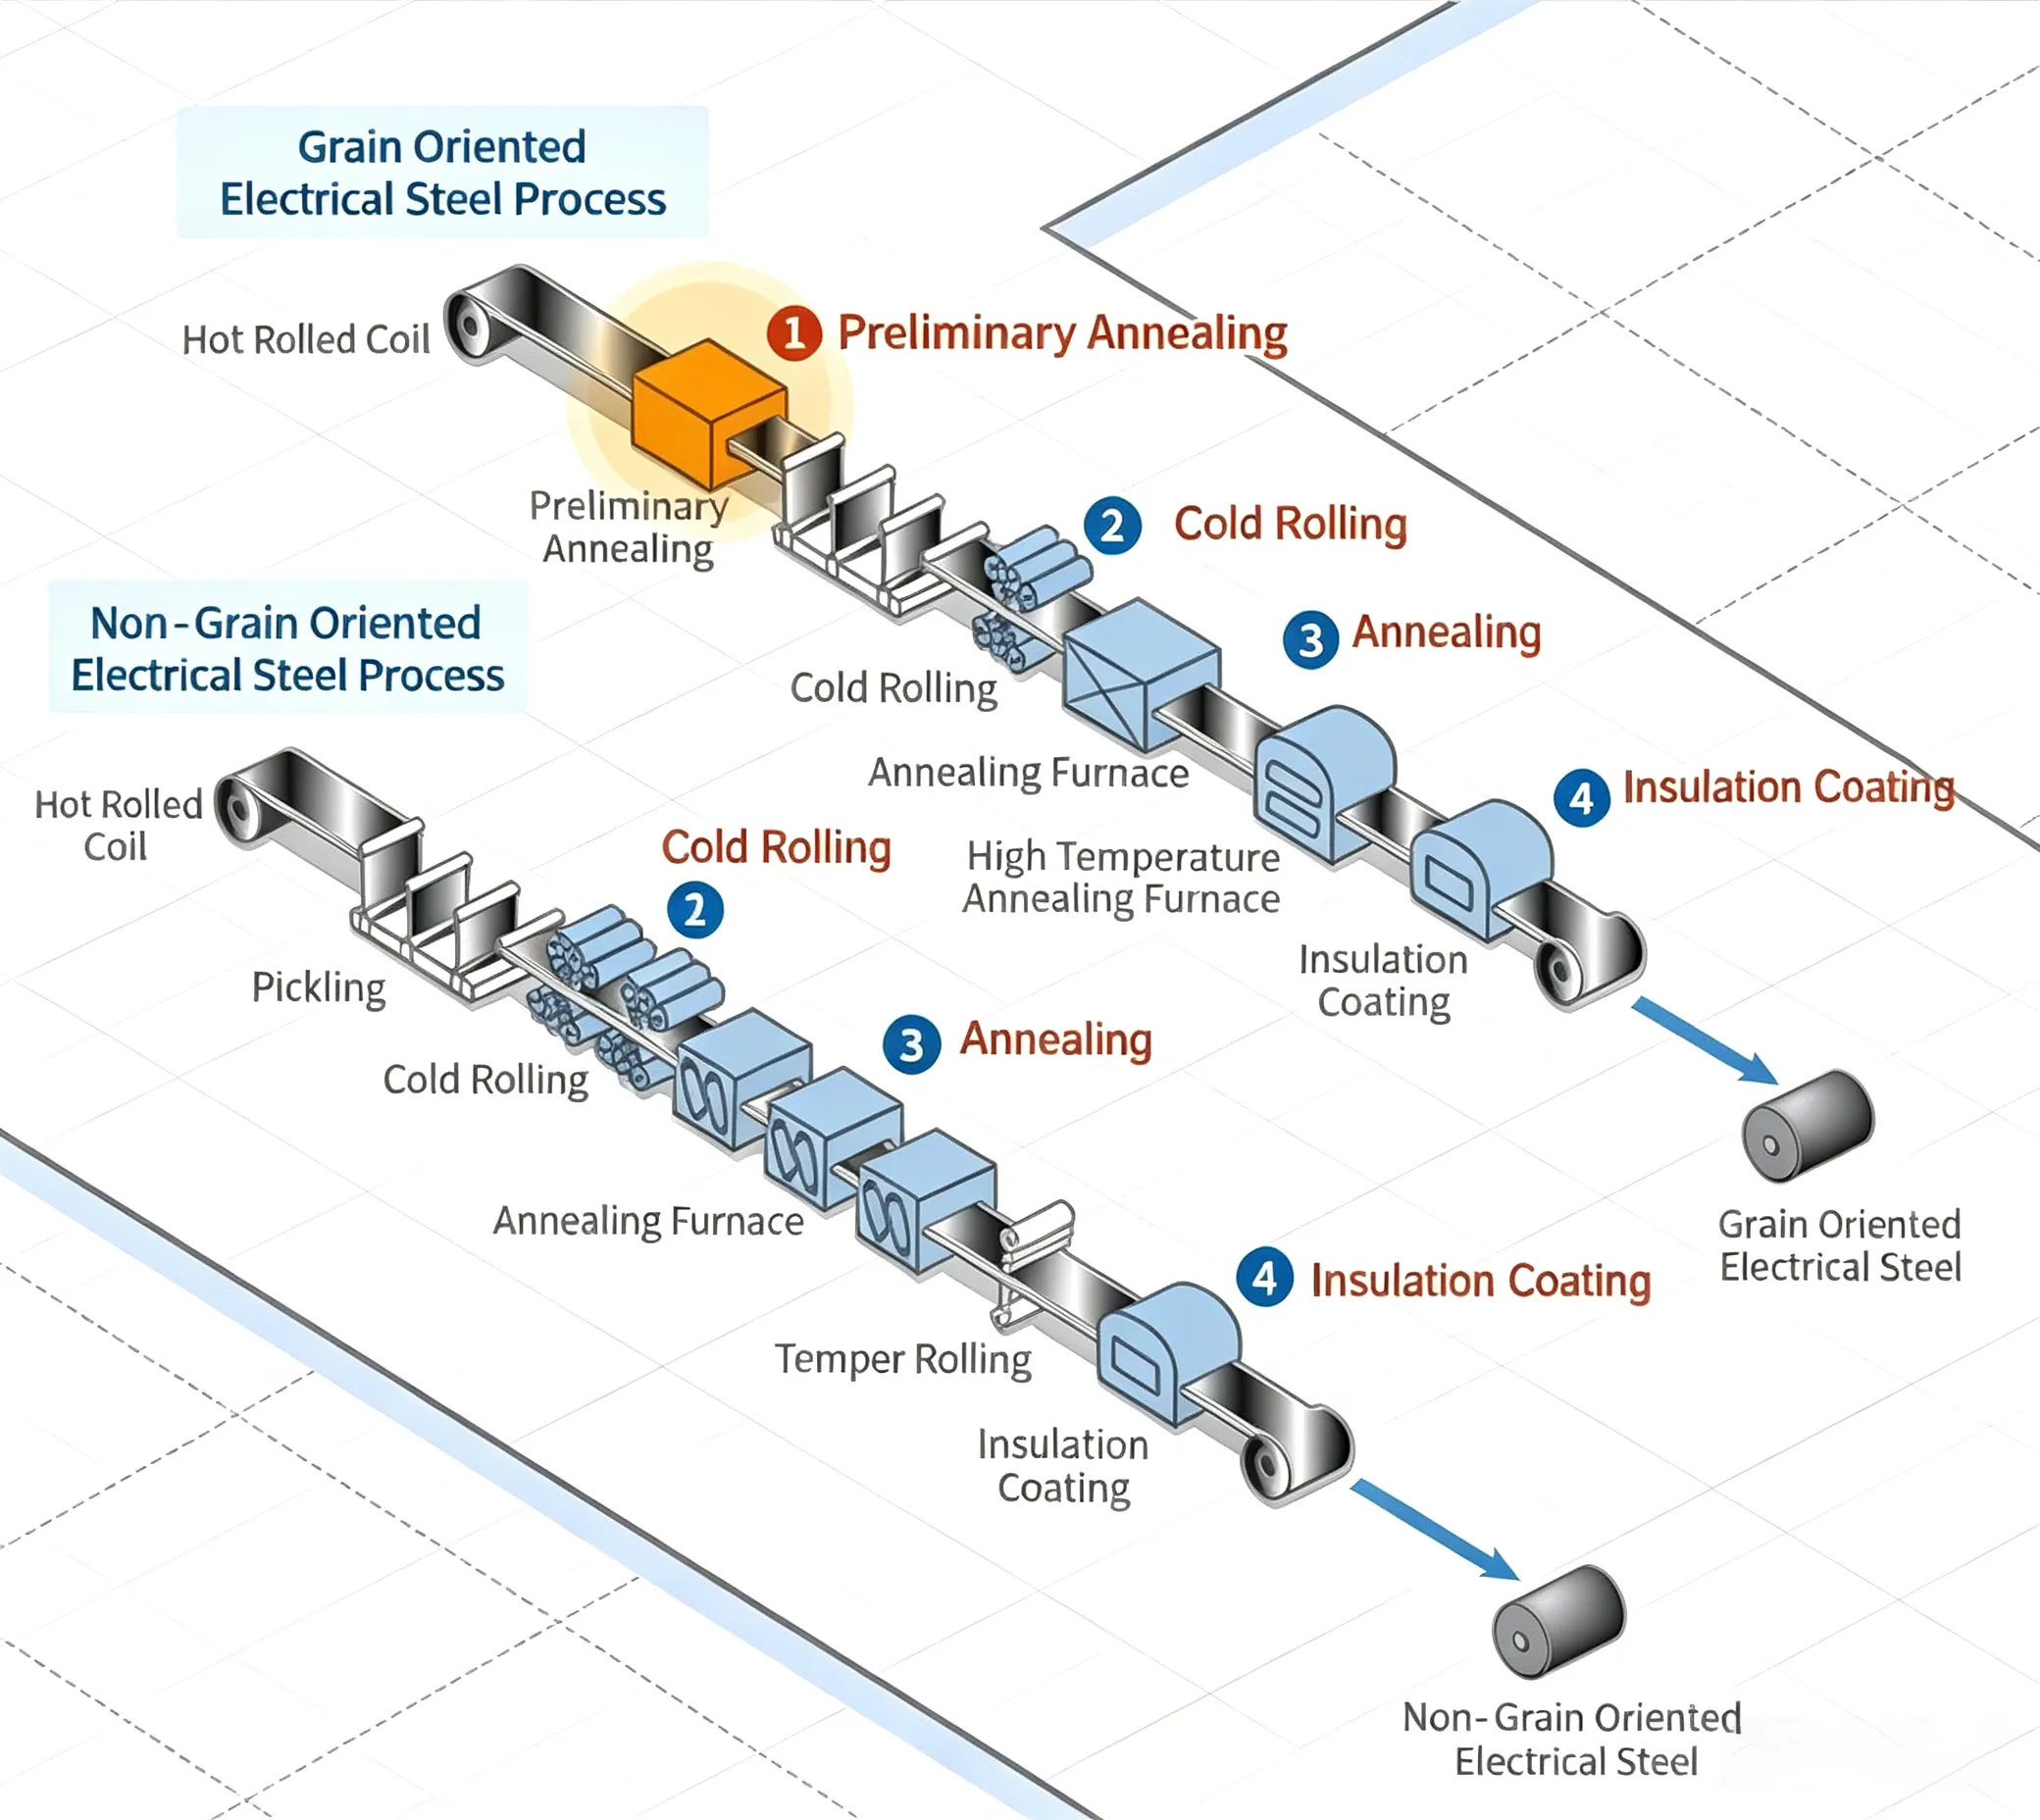
    During the preliminary annealing process, surface scale generated during hot rolling is effectively removed through scale breaking and hydrochloric acid pickling. This initial heat treatment improves the material’s cold rolling performance, refines the microstructure, and enhances the magnetic properties required for high-performance electrical steel production.
  2. Cold Rolling
    To achieve the required thickness, dimensional accuracy, and mechanical properties, cold rolling is performed with a typical reduction ratio of 40%–90%. Advanced rolling and automatic edge-trimming systems ensure precise control of strip thickness and width, delivering excellent dimensional consistency and surface quality.
  3. Annealing
    Annealing is a critical heat treatment process that transforms the cold-rolled structure into a fully recrystallized microstructure, optimizing the magnetic performance of electrical steel. For grain-oriented electrical steel (GOES), two key annealing processes are applied: decarbonization annealing and high-temperature annealing.
    Decarburization annealing removes excess carbon from the steel matrix and enables the formation of a uniform MgO coating, which acts as a key component in the high-temperature treatment process. Subsequent high-temperature annealing promotes secondary recrystallization, producing a highly oriented grain structure with excellent magnetic properties and low core loss.
  4. Insulation Coating
    An advanced insulation coating process is applied using continuous coating equipment to reduce eddy current losses and improve electrical efficiency. The coating thickness and composition are precisely controlled according to product specifications and application requirements.
    For grain-oriented electrical steel, a dual-layer coating system is typically applied, consisting of a dark brown forsterite (Mg₂SiO₄) base coating and a phosphate-based insulating top coating, providing excellent insulation performance, surface quality, and magnetic stability.
    For non-oriented electrical steel (NOES), customized insulation coatings with different thicknesses and compositions are selected based on specific application requirements, including motors, generators, transformers, and other electrical equipment.