INQUIRY

Manufacturing

Forging Steel
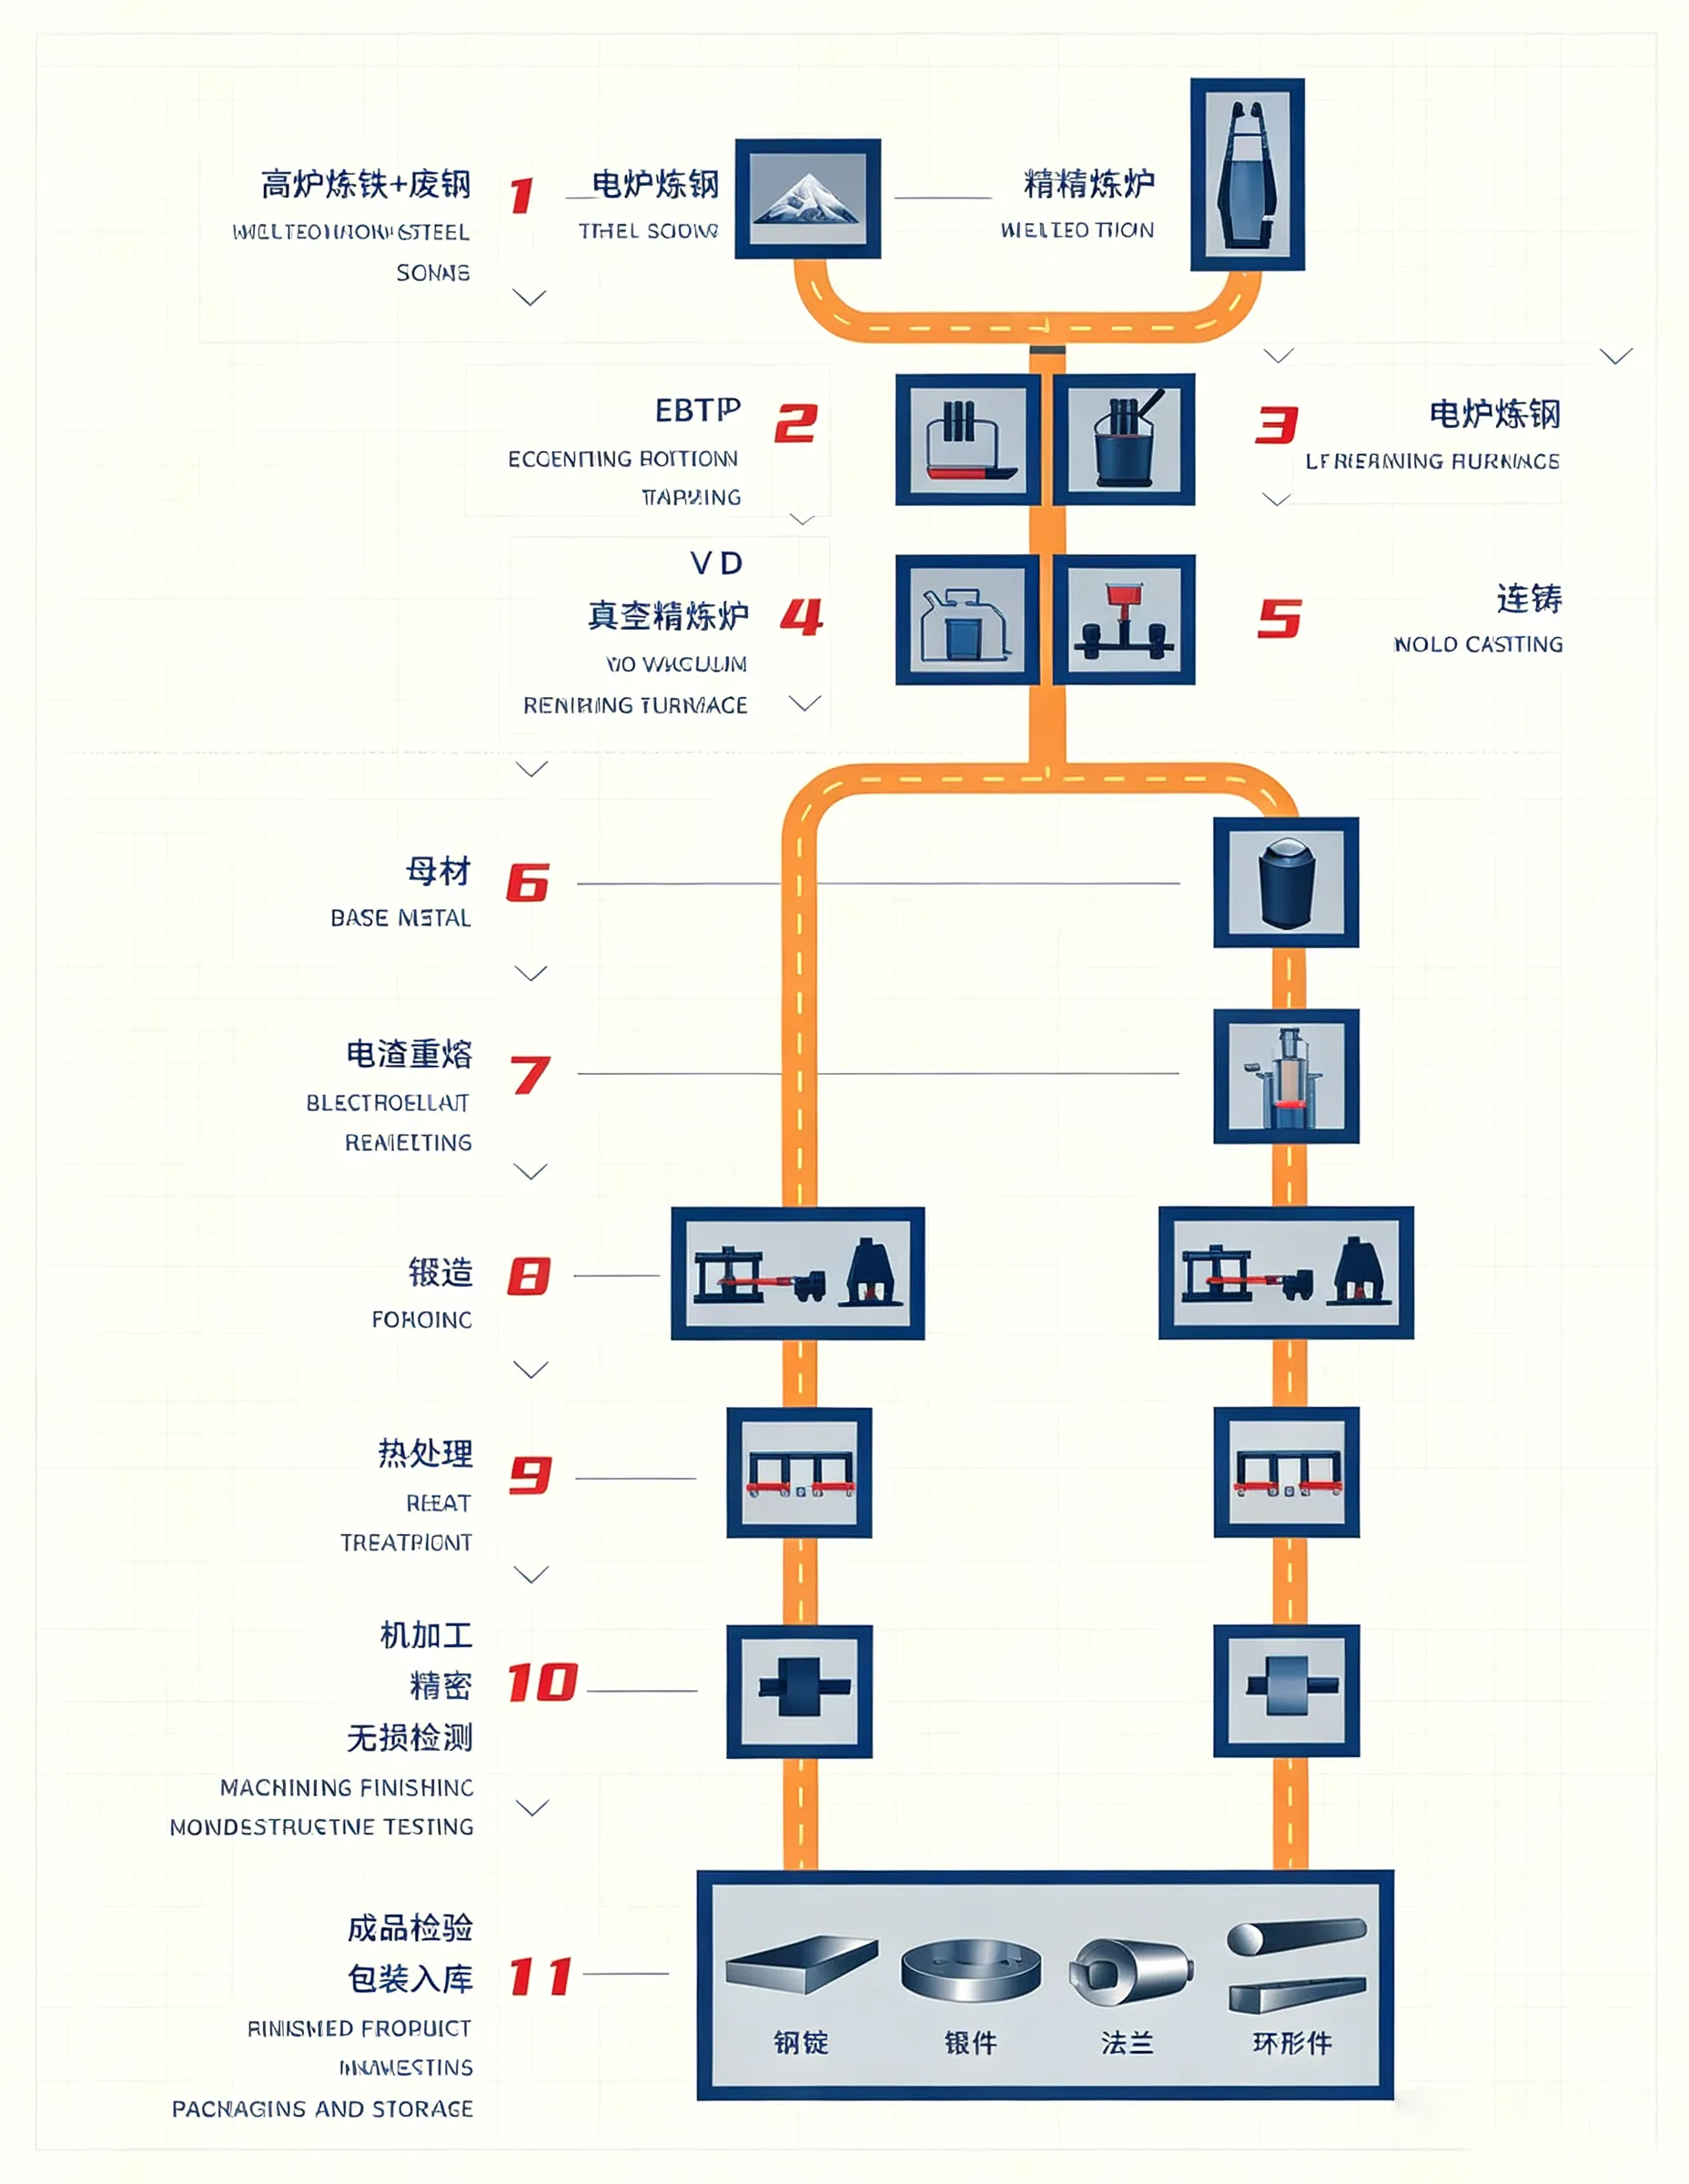
Forged Steel Manufacturing Process

1. Heating

The forging process begins with high-quality steel billets or ingots, which are selected according to the required component specifications and final product applications. The material is heated under precisely controlled furnace conditions to achieve the optimal forging temperature, allowing sufficient plasticity while maintaining structural integrity for subsequent deformation processes.

2. Preforming

During the preforming stage, heated billets undergo preliminary shaping through processes such as edging and blocking using hydraulic presses or forging hammers. Edging increases the effective cross-sectional area and improves material distribution, while blocking refines the preliminary shape and prepares the workpiece for final forging.

3. Finish Forging

In the final forging stage, the preformed workpiece is precisely formed within closed dies under controlled pressure. This process establishes the final geometry of the component while enhancing material density, mechanical strength, and structural uniformity. Depending on product complexity, multiple forging strokes and specially designed dies may be applied to achieve the required dimensions and performance.

4. Controlled Cooling

Controlled cooling is a critical process for optimizing the mechanical properties of forged steel. By carefully managing cooling rates, the grain structure and flow characteristics of the material are refined, resulting in improved strength, toughness, and fatigue resistance.

During closed-die forging, excess material known as flash flows outside the die cavity. As the flash cools and solidifies rapidly, it provides additional resistance that helps ensure complete die filling and improves the dimensional accuracy of the forged component.

5. Finishing and Surface Treatment

After forging, finished components undergo trimming, machining, and surface treatment processes to achieve the required dimensional accuracy and surface quality. Additional treatments, including surface protection and anti-corrosion processes, can be applied to enhance durability, corrosion resistance, and overall product appearance.
Wire Rod
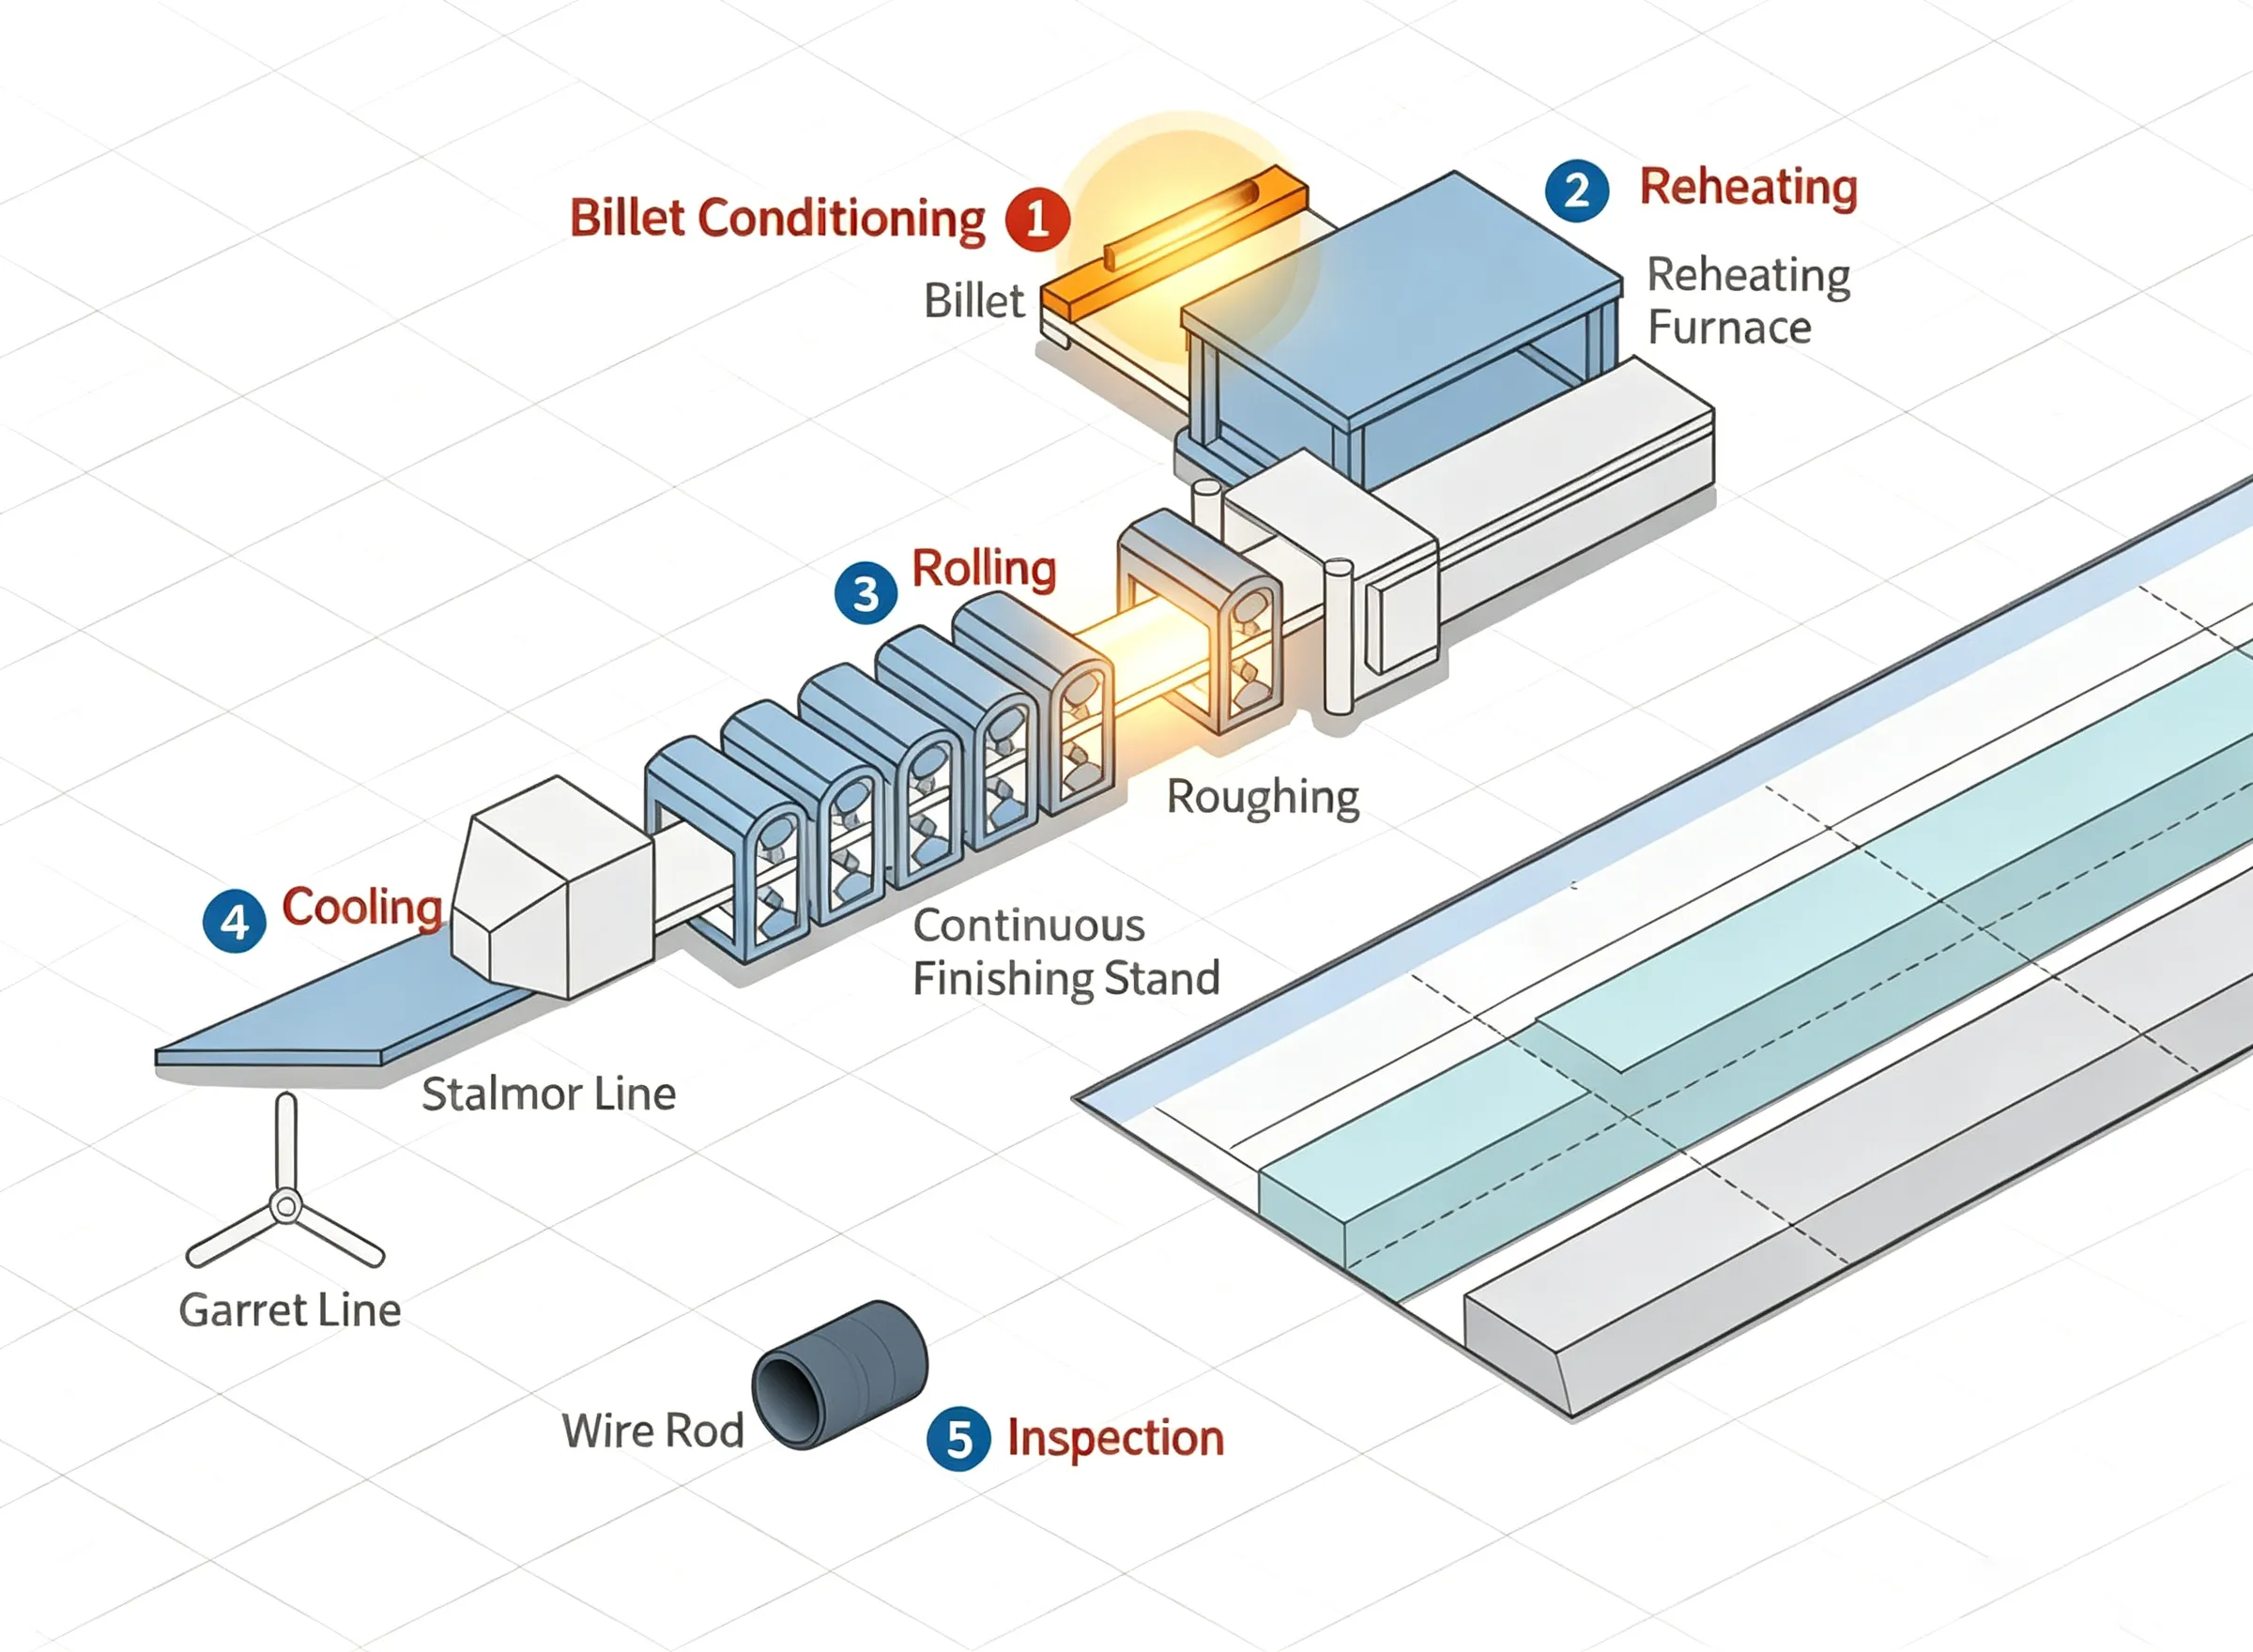
Wire Rod Manufacturing Process

1. Billet Conditioning and Quality Inspection:High-quality billets undergo comprehensive surface inspection and conditioning before rolling. Advanced shot blasting technology is applied to remove surface scale, while magnetic particle testing and visual inspection are conducted to identify surface defects. Any detected imperfections are eliminated through grinding. In addition, ultrasonic testing and dimensional analysis are performed to ensure internal quality control and verify billet integrity before production.
2. Reheating:Billets are precisely reheated under controlled furnace conditions to achieve the optimal temperature required for rolling. The reheating temperature and holding time are carefully adjusted according to the targeted product application. Advanced combustion control technology ensures an optimized fuel-to-air ratio, minimizing decarburization and preserving excellent surface quality and metallurgical properties.
3. Rolling:During the rolling process, key parameters including rolling temperature, reduction ratio, and deformation speed are precisely controlled to achieve the required mechanical properties and dimensional accuracy. Advanced rolling technologies, including optimized roll gap adjustment, roll surface control, crack detection, and dimensional correction systems, ensure superior surface quality and consistent product performance.
4. Controlled Cooling:After rolling, wire rods undergo controlled cooling through precise regulation of laying head temperature, cooling air flow, blower speed, and insulation cover cooling rates. The cooling process is optimized according to steel grade requirements to achieve the desired microstructure and mechanical properties.
5. Inspection and Packaging:Following rolling and cooling, finished wire rods undergo comprehensive quality inspections, including dimensional accuracy, surface condition, and material integrity testing. Samples from both the front and rear sections of the coil are evaluated to ensure compliance with customer specifications. Final packaging, labeling, and product identification are carefully inspected before shipment to guarantee safe delivery and traceability.

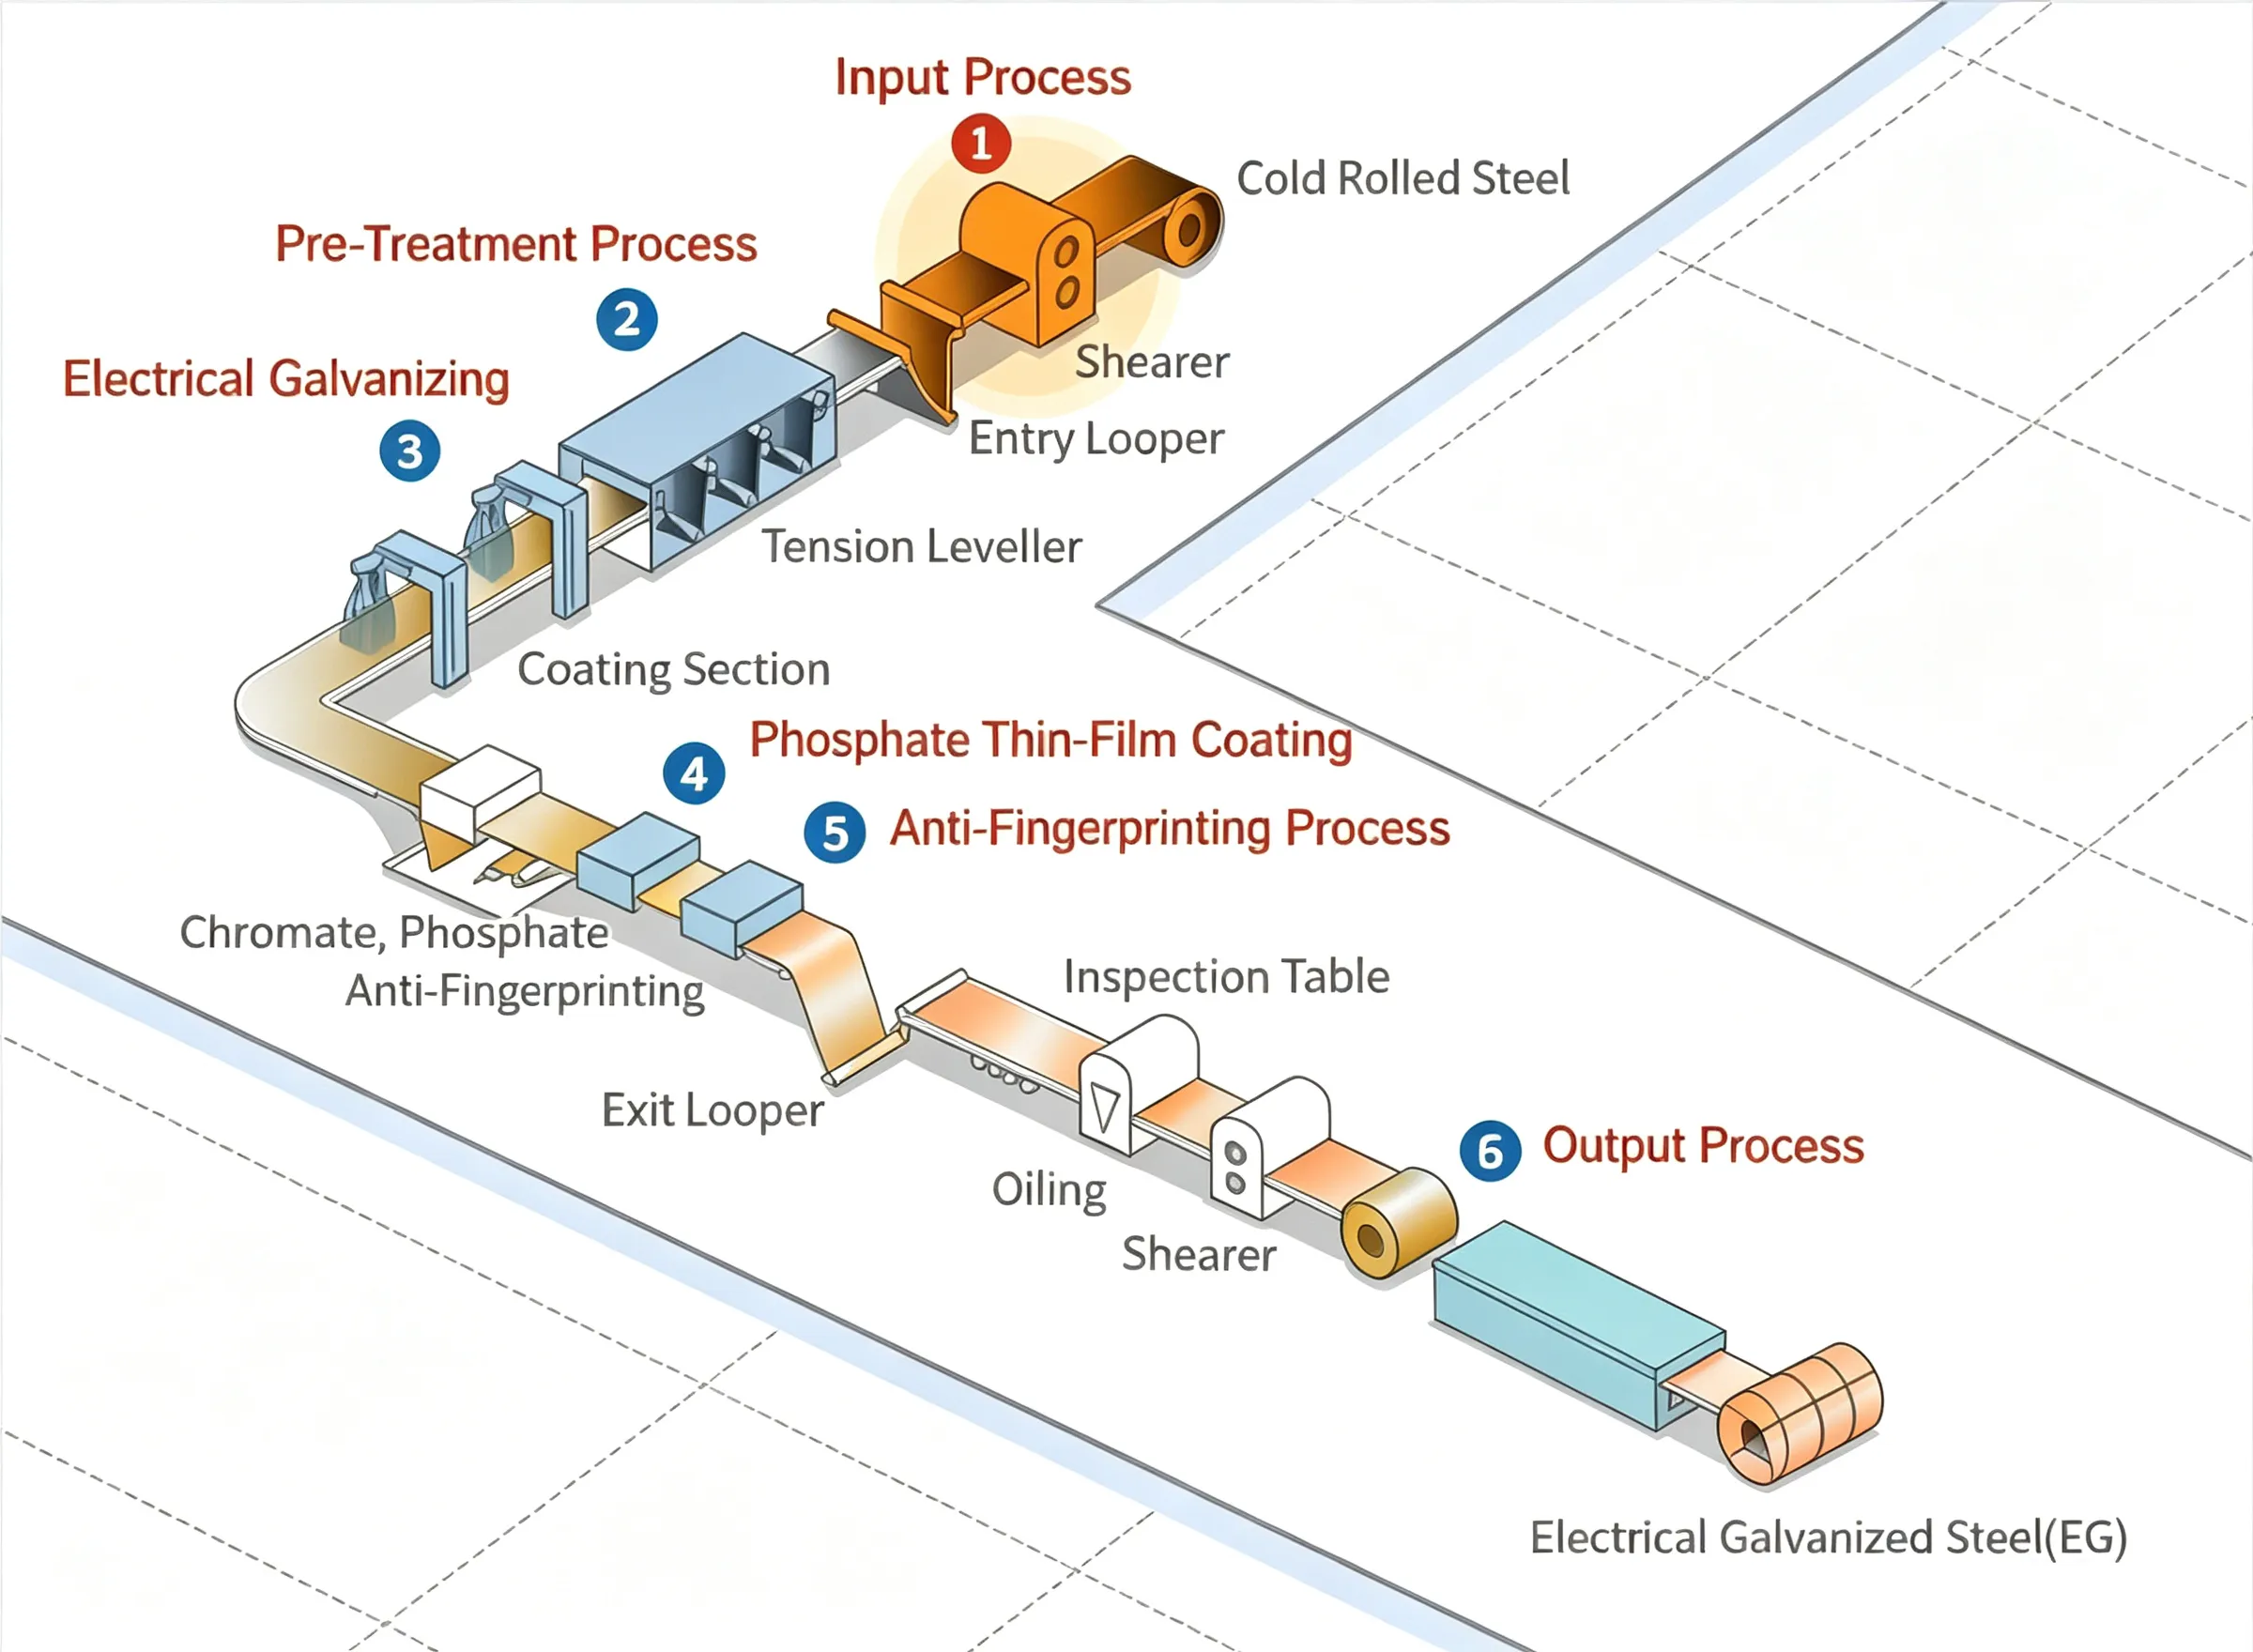
2 Electrical Galvanized Steel
Electro Galvanized Steel Manufacturing Process

1.Input and Strip Joining Process:The entry section of the electro galvanizing line is equipped with advanced production units, including a pay-off reel, shear machine, welding machine, looper, and tension leveler. Steel coils, including cold-rolled materials, are continuously fed into the line, accurately cut, and joined through automatic welding to ensure stable and uninterrupted production.
2.Pre-Treatment Process:Before electro galvanizing, steel sheets undergo a comprehensive electrolytic cleaning process consisting of electrolytic cleaning tanks, acid pickling sections, and rinsing systems. This process effectively removes surface contaminants, residual oils, and oxide films, creating a clean and activated surface to ensure excellent coating adhesion and uniform plating quality.
3.Electro Galvanizing Process:SHOUYUAN applies advanced electro galvanizing technologies, including the CAROSEL plating method, in which zinc coating is deposited onto the steel surface through controlled electrochemical reactions using conductor rolls. This process enables the production of single-sided, double-sided, and differential-coated steel sheets with precise coating control.
In addition, horizontal electro galvanizing technology allows simultaneous plating on both sides of the steel sheet, ensuring uniform coating distribution and meeting diverse customer requirements.
4.Phosphate Thin-Film Coating:A phosphate conversion coating is applied to the zinc surface through chemical or electrochemical treatment. This thin protective film provides temporary corrosion protection while improving paint adhesion and creating an ideal surface for subsequent coating and painting processes.
5.Anti-Fingerprint Treatment:To further enhance surface performance, an organic, inorganic, or organic-inorganic hybrid coating is applied to the galvanized steel surface. This treatment improves corrosion resistance, fingerprint resistance, surface appearance, and processing performance, making the products suitable for applications requiring high-quality surface finishes.
6. Output and Packaging Process:At the exit section of the production line, finished galvanized coils pass through an output looper, tension reel, and automated packaging system. These processes ensure stable coil formation, product protection, and safe handling before delivery to customers.

Spiral Welded Pipe (SSAW)
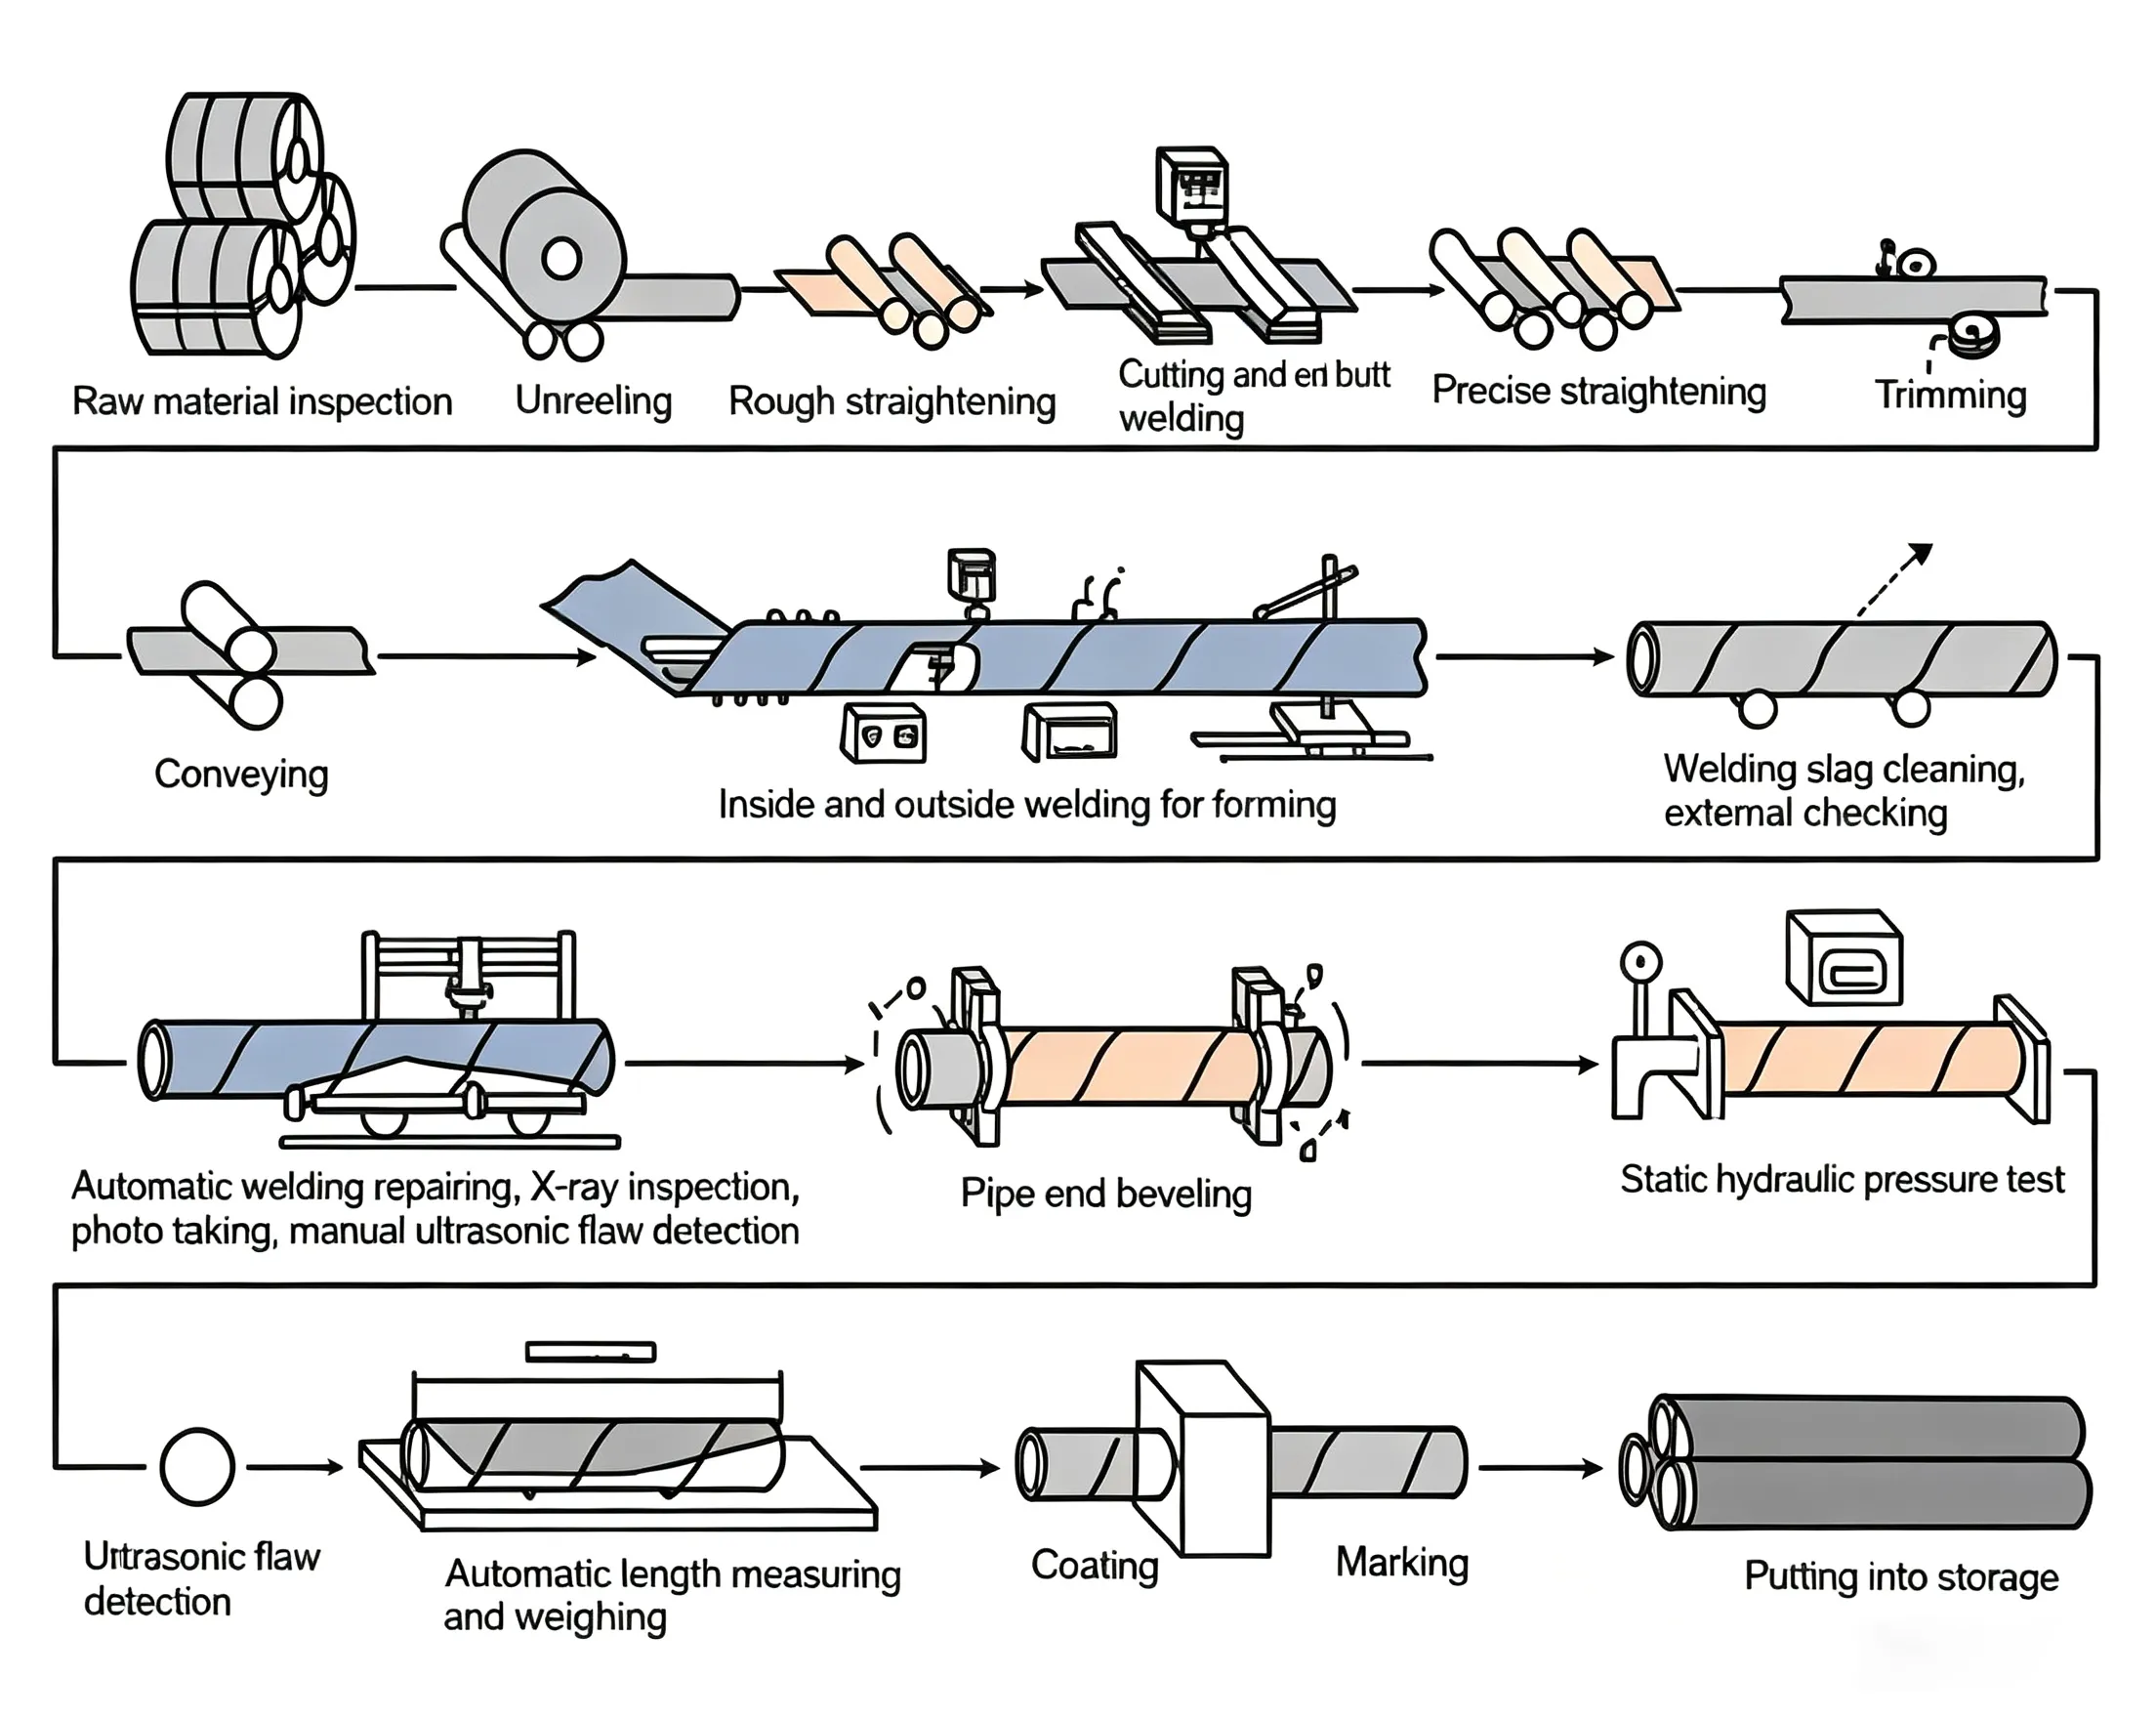
Spiral Submerged Arc Welded Pipe (SSAW) Manufacturing Process

1. Uncoiling and Straightening:High-quality steel coils are carefully selected and processed through advanced straightening equipment to achieve excellent flatness and dimensional accuracy. This process provides a stable foundation for subsequent forming and welding operations, ensuring consistent pipe quality.

2.Forming:During the forming process, steel strips are gradually shaped into a cylindrical pipe through multiple forming rolls. Precise control of roll positioning, forming speed, and alignment parameters ensures accurate pipe diameter, uniform wall thickness, and reliable dimensional consistency.

3.Internal and External Welding:SHOUYUAN utilizes advanced submerged arc welding (SAW) technology and double-sided welding systems to perform high-quality internal and external welds. Automated welding control and tracking systems continuously monitor welding parameters, ensuring strong, reliable, and defect-free weld seams.

4.Pipe Cutting:After welding, pipes are accurately cut to the specified lengths using advanced cutting technology. This process ensures precise dimensions and meets customer requirements for different application standards.

5.Inspection and Quality Control:Comprehensive quality inspections are conducted using advanced testing technologies, including ultrasonic flaw detection and X-ray inspection systems, to verify weld integrity and overall pipe performance. Any detected defects are promptly repaired and re-inspected to ensure that every pipe meets required quality standards.

6.Pipe End Processing and Anti-Corrosion Treatment:Finished pipes undergo surface cleaning to remove oil, impurities, and contaminants. Advanced coating and spraying technologies are then applied for anti-corrosion protection, significantly enhancing service life and durability. Through strict processing and quality control procedures, high-performance spiral welded pipes are delivered to meet demanding industrial applications.